
Case study 1 · Dubai, UAE · Filler masterbatch
Filler masterbatch extruder that would not hold spec: three days in Dubai
A PE filler masterbatch producer in Dubai ran a KTE-75B at 560 rpm to chase output and got yellowed, porous pellets instead. The filler masterbatch extruder was not rebuilt — screw speed, barrel profile, die temperature and the vacuum vent were reset, and the line came back inside specification in three days.
Quick answer
The filler masterbatch extruder was being run like a virgin-resin line. Screw speed had been pushed to 560 rpm to chase tonnage, which put melt temperature about 25 °C above the window a PE carrier tolerates and left the vacuum vent with nothing to pull. Dropping to 400–430 rpm, lowering the barrel profile 15–20 °C, raising the die to 180–185 °C and pulling −0.08 MPa at the vent put pellets back inside spec at 600–650 kg/h on 80% CaCO3 — no screw element, barrel or die was replaced.
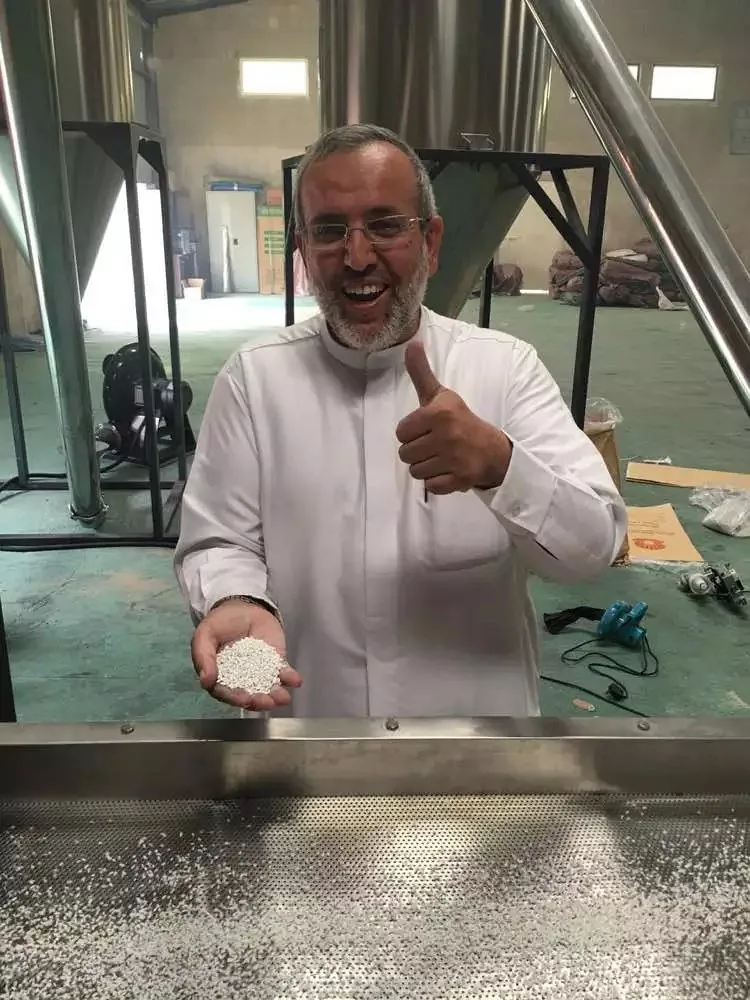
Photograph from the commissioning file for this project; customer names are withheld where requested.
The situation: good output, rejected pellets
The customer is a filler masterbatch producer supplying film and injection moulders around the Gulf. The line is a KTE-75B — 71 mm screws, 2×1,530 N·m, 132–160 kW, quoted for 300–800 kg/h — feeding 1,250-mesh coated CaCO3 at 80% into an LLDPE carrier, water-ring hot-face cutting, centrifugal dryer, bagging.
Output was there. What was not there was the product: pellets came out with a yellow cast, a rough surface and visible porosity, and the customer's film line blew holes at 40 µm. Their first conclusion was that the filler masterbatch extruder was undersized for 80% loading. Their second was that the CaCO3 supplier had changed the coating. Both were wrong.
What the readings showed on a filler masterbatch extruder
An engineer was on the site three days after the call (visa included). The first hour was spent reading the panel rather than the pellets, because the symptom — yellow, porous, rough — has three different causes and they were all present at once.
| Reading | On arrival | Target | What it explained |
|---|---|---|---|
| Screw speed | 560 rpm | 400–430 rpm | Specific energy up ~30%; filler-filler friction heats the melt faster than the barrels can cool it. |
| Melt temperature | 212 °C | 185–192 °C | Yellow cast and smell: the LLDPE carrier is degrading, not the CaCO3. |
| Barrel profile | 190 °C flat, all zones | 165 → 185 °C falling | Feed zone too hot: powder bridges at the throat, throughput surges and starves. |
| Die temperature | 170 °C | 180–185 °C | Die pressure high, strand surface torn, die holes partially frozen. |
| Vacuum at vent | −0.02 MPa | −0.06 to −0.09 MPa | Mineral carries 0.3–0.5% moisture in Gulf humidity; that is the porosity. |
| Feeder | Volumetric, uncalibrated | Gravimetric, ±0.5% | Loading drifting 78–83%: density and dispersion wander with it. |
The important finding is the one that is easy to miss: above roughly 75% filler, screw speed stops being an output lever. The melt is already torque-limited, so the extra 130 rpm bought almost no tonnage — it only added shear heat. The customer had been turning the only knob they had.
What we changed, in the order it was changed
- Speed down first, output measured after. 560 → 420 rpm, then a torque and melt-temperature check at each step. Output fell 8% and then came back as the profile was corrected — the line had been running against its own cooling capacity.
- Barrel profile inverted. From a flat 190 °C to a falling profile, 165 °C at the feed throat rising to 185 °C before the die. Cool feed zone ends the bridging; the shear heat does the melting, which is what a high-filler compound needs.
- Die up to 180–185 °C. High-filler melt needs a hot die to pass the holes without tearing the strand surface; the previous setting was borrowed from a 60% formulation.
- Vacuum opened to −0.08 MPa. The vent had been running at −0.02 MPa, which is enough to hold a seal and not enough to remove the moisture the mineral brings in. Porosity disappeared in the same shift.
- Feeder calibrated and locked. Loss-in-weight verified against a 10-minute catch sample; the loading figure the customer quotes to their own customers is now the loading the line actually runs.
Result
Pellets came back inside the customer's own incoming inspection — colour, surface, and film blown at 40 µm without holes — at 600–650 kg/h on 80% CaCO3, which is inside the band the KTE-75B is quoted for. No screw element, barrel liner or die was replaced, and no formulation change was made.
Line configuration
| Stage | Equipment | In this case |
|---|---|---|
| Main machine | KTE-75B, 71 mm, 2×1,530 N·m, 132–160 kW | Unchanged; settings only |
| Screw geometry | 45°/90° kneading blocks, W6Mo5Cr4V2 elements, bimetallic liner | Unchanged; the wear check showed 0.3 mm on the first mixing block |
| Feeding | Loss-in-weight on the mineral, volumetric on the carrier | Both calibrated; carrier feeder scheduled for gravimetric upgrade |
| Devolatilization | Vacuum vent at barrel 7 | −0.02 → −0.08 MPa |
| Pelletizing | Water-ring hot-face, centrifugal dryer, vibrating screen | Water 45–55 °C, die 180–185 °C |
What transfers to your line
If you run 75–85% CaCO3 or talc on a twin screw, the sequence above is the first thing to check on your filler masterbatch extruder before you accept a quotation for a bigger machine:
Three readings that decide the case
Melt temperature against carrier limit — above it, yellowing is chemistry, not colour. Vacuum level at the vent — below −0.06 MPa, porosity at 80% loading is a vent problem, not a dispersion problem. Specific energy (kWh/kg) — if it climbs while output does not, you are heating the compound, not making it.
The same correction applies to talc, which is harder to wet out and more abrasive: the temperature window is similar but the screw geometry and the wear package are not. The talc filler masterbatch page covers that difference, and the CaCO3 page carries the parameter table this case was checked against.
FAQ
Why did higher screw speed not raise output on this filler masterbatch extruder?
Because above roughly 75% filler the line is torque-limited, not volume-limited. The screws are already full; turning them faster adds shear heat without adding conveying capacity. On this line the extra 130 rpm cost about 25 °C of melt temperature and bought under 5% output.
Was the CaCO3 the problem?
No. Coating and mesh were checked against the incoming certificate and were unchanged. The moisture the mineral carried (0.3–0.5%) only became a defect because the vent was running at −0.02 MPa instead of −0.08 MPa.
Would a bigger machine have fixed it?
It would have hidden it. A larger filler masterbatch extruder run at the same flat 190 °C profile and the same weak vacuum would have produced the same yellow, porous pellets at a higher capital cost. The settings were the defect: a bigger machine would have repeated them.
How long does a commissioning visit like this take?
Three to five days for a single line with material on site: one shift to read the panel and pull a sample, one to change and verify settings, and the rest to train the shift leaders so the settings survive the visit. Visa time is separate and depends on the country.
Where this record comes from
Commissioning reports, service logs and the parameter sheet issued with the line. Machine figures are the quoted bands for the model; process windows follow the Kerke parameter table and are confirmed on a material trial before they become a production setpoint. Where the customer asked not to be named, the country and the application are kept and the company name is not.
Reviewed by the Kerke process team, Nanjing. Case published 9 November 2026.
Send 25–50 kg and we run it on our lab extruder: pellets, running video and a capacity report back in 3–7 days.
Filler masterbatch extruder — the short version
Note on filler masterbatch extruder: the readings in this record come from the commissioning log of the line described, and the settings are the ones that were left with the customer. Treat them as a starting point for your own material, not as a guarantee — the same correction on a different filler grade or carrier ends in a different number.
Related on this site: Extrusion lines by application · Twin screw extruder types · free extrusion line quotation · Wikipedia: Extrusion