
Case study 9 · Mexico · PA + short glass fibre
PA glass fiber compounding on a KTE-75D: shipping damage solved in two days
A compounder in Mexico bought a KTE-75D for PA with short glass fibre. The container arrived with damage; photographs went over the same day and the replacement parts left the factory within two. The harder part of PA glass fiber compounding was not the shipping — it was the drying and the side feeder, and both were set before the first run.
Quick answer
PA glass fiber compounding fails on two things: moisture in the resin and fibre broken at the side feeder. This KTE-75D (71 mm, 2×2,100 N·m, 500–1,000 kg/h) runs dried PA at 120 °C for 4 hours, feeds 20–50% glass downstream at barrels 4–6, keeps L/D 44–52 with a bimetallic barrel, and strand-cuts through a die shaped to avoid aligning the fibre. When the container arrived damaged, the parts were replaced in two days, so the schedule held.
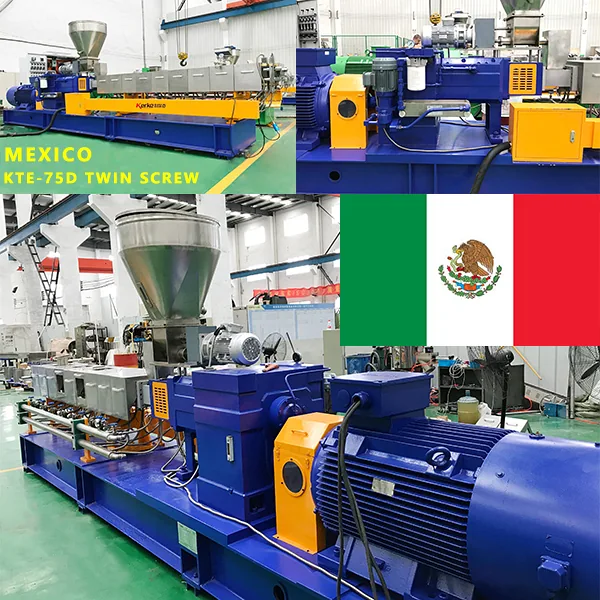
Photograph from the commissioning file for this project; customer names are withheld where requested.
The situation: a high-torque line and a damaged container
The customer compounds engineering plastics in central Mexico, mainly PA6 and PA66 with short glass fibre for automotive and electrical customers. The machine is a KTE-75D: 71 mm screws, 2×2,100 N·m and 200–315 kW, quoted for 500–1,000 kg/h — the D-series torque class is what makes 30–35% glass at that output possible without running out of torque in the mixing zone.
Shipping is the part of an export order nobody controls. The container was handled badly in transit and part of the shipment arrived damaged. The customer photographed it and sent the images the same day; the parts were in a crate and on their way within two days, which kept the installation schedule intact.
What decides quality in PA glass fiber compounding
Glass-filled PA is judged on impact strength, and impact strength is mostly fibre length. Everything in the line either protects fibre length or destroys it.
| Stage | Risk | Setting on this line |
|---|---|---|
| Resin drying | PA absorbs moisture; hydrolysis drops molecular weight and impact | 120 °C × 4 h, moisture below 0.1% before the hopper |
| Glass feeding | Feeding into a starved or partly melted section breaks rovings | Side feeder at barrels 4–6, after the melt is complete; 2–3 feed points for 30% and above |
| Screw after the side feeder | 90° kneading blocks chop the fibre | Large-lead conveying and moderate shear; toothed elements rather than 90° blocks |
| Die and cutting | Die shape aligns fibre, then the cutter snaps it | Die designed for low orientation; strand cut with a water bath, not die-face |
| Wear | Glass abrades the flight tips and barrel wall | Bimetallic barrel, PM screw elements, wear check on schedule |
Two of these are decisions made at quotation for any PA glass fiber compounding line, not at commissioning: the D-series torque class and the wear package. A B-series machine at the same diameter will run 30% glass, and it will run out of torque before it runs out of die pressure — which shows up as a line that cannot reach its quoted output on a hot day.
What was done on site
- Damage assessed from photographs the day the container was opened: barrel heating zone cover, one die plate, a section of the water bath frame. None of it structural.
- Replacement dispatched within two days, from stock rather than from a production queue — the reason the schedule held.
- Drying verified before the first run. The customer's dryer was checked against a moisture reading; a dryer that is 15 °C low looks fine and ruins the compound.
- Side feeder position and rate set. Glass at barrels 4–6, feed rate ramped until the melt temperature and torque settled, then locked.
- Strand line and die set. Bath distance and water temperature adjusted for the PA grade; pellets checked for fines and for fibre tufts on the cut face.
Result
The PA glass fiber compounding line reached its quoted output on 30% glass with impact values inside the customer's specification, and the installation finished on the original date despite the container damage. The customer's assessment was about the response rather than the machine:
Line configuration
| Item | Specification |
|---|---|
| Model | KTE-75D, 71 mm, 2×2,100 N·m, 200–315 kW |
| Output band | 500–1,000 kg/h (PA66 + 30% GF) |
| L/D | 44–52 |
| Glass feeding | Side feeder at barrels 4–6, 20–50% loading |
| Wear package | Bimetallic barrel, PM screw elements |
| Filtration | 40–80 µm screen changer |
| Pelletizing | Water-bath strand, centrifugal dryer |
What transfers to your line
Three things to specify before the quotation, not after
Torque class — D-series for 30% glass and above at tonnage, because B-series runs out of torque before it runs out of die. Wear package — bimetallic barrel and PM elements; glass is a grinding medium, not a filler. Side feeder position — barrels 4–6, after complete melting; feeding glass into unmelted resin is the fastest way to lose fibre length.
The parameter set is on the glass fibre compounding page; drying, drying and drying are covered again in the troubleshooting article, because it is the cause of most "the machine changed" complaints on PA.
FAQ
What glass loading can a KTE-75D run?
20–50% short glass, with 30–35% being the common automotive and electrical specification. Above 40% the die, the wear package and the cutting method all change, and the quotation should say so.
Why does fibre length matter more than glass content in PA glass fiber compounding?
Because impact strength tracks fibre length, not the percentage on the certificate. A 30% compound with intact fibre outperforms a 35% compound where the side feeder and the screw after it have chopped the glass.
Which pelletizing method for glass-filled PA?
Water-bath strand cutting on a PA glass fiber compounding line, with a die designed to avoid aligning the fibre. Die-face cutting snaps fibre at the die and gives a dustier pellet; it is used where the compound allows it, not as a default.
What happens if the container arrives damaged?
Photograph everything before unloading, send the images the same day, and ask for the parts list by position. On this order the replacements were dispatched within two days from stock, which is why the installation date did not move.
Where this record comes from
Commissioning reports, service logs and the parameter sheet issued with the line. Machine figures are the quoted bands for the model; process windows follow the Kerke parameter table and are confirmed on a material trial before they become a production setpoint. Where the customer asked not to be named, the country and the application are kept and the company name is not.
Reviewed by the Kerke process team, Nanjing. Case published 9 November 2026.
Send 25–50 kg and we run it on our lab extruder: pellets, running video and a capacity report back in 3–7 days.
Pa glass fiber compounding — the short version
Note on pa glass fiber compounding: the readings in this record come from the commissioning log of the line described, and the settings are the ones that were left with the customer. Treat them as a starting point for your own material, not as a guarantee — the same correction on a different filler grade or carrier ends in a different number.
Related on this site: Extrusion lines by application · Twin screw extruder types · free extrusion line quotation · Wikipedia: Extrusion