
Case study 5 · Germany · Graphite, ABS/HIPS, pencil
Graphite compounding line, ABS, HIPS and a pencil line: three weeks in Germany
A German compounder bought five machines at once — KTE-20, KTE-36B, KTE-50B, KTE-65B and an SE-30 — for graphite compounds, ABS and HIPS granules and a pencil line. Normal installation is a week; this took three, and the graphite compounding line was the one that taught everybody the most.
Quick answer
Five lines, three material families, one installation team. The graphite compounding line set the schedule: graphite is light (0.3–0.6 g/cm³ bulk), dusty, conductive and abrasive, so it is side-fed with a crammer, the whole line is grounded, and the wear package is specified before the first tonne. ABS and HIPS only needed drying and a gentler profile; the pencil line was a filled PS rod on an SE-30 single screw.
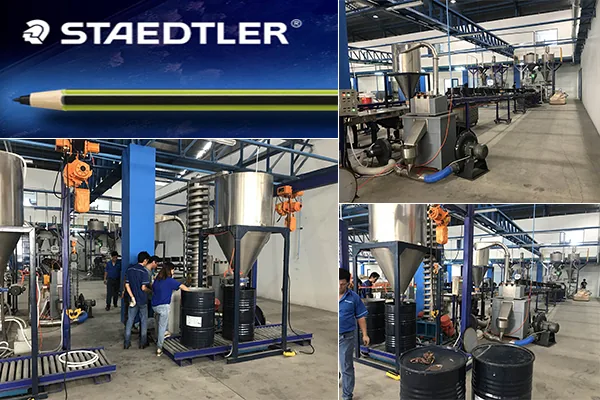
Photograph from the commissioning file for this project; customer names are withheld where requested.
The situation: one order, five machines, three products
This customer compounds in southern Germany and was bringing several small product lines in-house at once: graphite-filled compounds for thermal and electrical applications, ABS and HIPS granules for their own conversion, and a pencil line — a filled polystyrene rod, extruded and shaped, which is a compounding job wearing a different hat.
The order was a KTE-20 for development, a KTE-36B, a KTE-50B and a KTE-65B for production, and an SE-30 single screw for the pencil rod. Our normal installation window is one week per site. This one took three, and no single line was the reason — five lines sharing one compressed-air supply, one chiller and one operator team is a scheduling problem before it is an engineering one.
What the graphite compounding line needed that the others did not
Graphite is the opposite of a mineral filler in the way it behaves upstream of the screw. It is light enough to float, it bridges, it coats everything with conductive dust, and it wears a screw. Those four facts set the configuration.
| Product | Machine | Constraint that decided the build |
|---|---|---|
| Graphite compounds | KTE-36B / KTE-50B | Bulk density 0.3–0.6 g/cm³, so the filler is side-fed with a crammer; conductive dust means grounding and sealed cabinets; abrasive means bimetallic liner and a wear-check interval. |
| ABS / HIPS granules | KTE-50B / KTE-65B | Drying at 80–90 °C for 3–4 h; a gentle profile because both polymers are sensitive to over-shearing at the die. |
| Pencil rod | SE-30 single screw + die | Filled PS through a rod die: pressure stability and die temperature matter more than mixing, which is why it is a single screw duty. |
The graphite line's feeding arrangement is the part most buyers underestimate. A volumetric feeder on graphite will run, and it will run at a loading that drifts by several percent as the hopper empties and the material compacts. A crammer-fed side feeder holds the ratio, and the ratio is the product — conductivity is sold as a specification, not as an average.
How the three weeks were spent
- Week 1 — mechanical and utilities. Five lines set, levelled and piped; one chiller loop shared, which needed a manifold and flow meters per line before anything was started.
- Week 2 — the graphite compounding line. Side feeder and crammer calibrated, grounding verified, first compound run at three loadings, wear inspection after the first 20 hours.
- Week 3 — ABS/HIPS and the pencil line. Drying verified, profiles set, rod die centred and the downstream haul-off matched to die swell; operator training on all five.
Two things came out of week 2 that were not in the original plan: a dust extraction point at the side-feeder throat, and a revised start-up order so the graphite line is cleaned before the ABS line runs, not after. Both are cheap on site and expensive in a production week.
Result
All five lines were accepted at the end of the three weeks. The graphite compounding line runs at the loading the customer sells to, the ABS/HIPS lines produce granules inside their incoming specification, and the pencil line — the one product nobody expected to be straightforward — came out ahead of the sample the customer had approved.
Line configuration
| Line | Machine | Role on site | Reference band |
|---|---|---|---|
| Development | KTE-20 lab twin screw | Formulation trials before a production run | lab scale |
| Graphite | KTE-36B, 2×720 N·m class | Small-lot conductive compounds | 80–200 kg/h |
| Graphite / ABS | KTE-50B, 50.5 mm, 2×525 N·m | Main compounding | 80–200 kg/h |
| ABS / HIPS | KTE-65B, 62.4 mm, 2×860 N·m | Volume granulation | 200–450 kg/h |
| Pencil rod | SE-30 single screw + rod die | Filled PS profile | set by die and haul-off |
What transfers to your line
Graphite is a feeding problem before it is a mixing problem
Bulk density 0.3–0.6 g/cm³ means the filler volume is several times the resin volume — a volumetric feeder will not hold the ratio. Conductive dust means grounding, sealed cabinets and a dust extraction point at the feeder throat, not a broom. Wear means a bimetallic liner and a scheduled inspection, because graphite is abrasive in a way that CaCO3 is not.
On this graphite compounding line the mixing side is comparatively easy: graphite wets out readily and does not need 90° dispersive blocks. If you are also running ABS or HIPS on the same site, keep the cleaning order — graphite before styrenics — or the first hundred kilos of the next product will carry black specks.
FAQ
Can one graphite compounding line run ABS and HIPS as well?
Yes — with a cleaning cycle between grades and a different screw set for the filled and unfilled duties. On this site the graphite and styrenic lines were separate machines because the volumes justified it; a single line is normal at lower tonnage.
Why is the pencil line a single screw and not a twin screw?
Because the job is pressure and shape, not mixing. A filled PS rod through a die needs stable pressure and a controlled die temperature; an SE-30 does that with less wear and a lower price than a twin screw of the same output.
How long should installation take for a multi-line order?
One week per line is the normal figure for a graphite compounding line or a styrenic line. Five lines on one site took three weeks because utilities, chiller capacity and operator training were shared — plan the utilities before the machines arrive and the schedule holds.
What wear package does graphite need?
Bimetallic barrel liner and hardened screw elements as a minimum, with the first inspection at about 20 running hours and then on the normal schedule. Graphite is abrasive and slightly conductive, so wear shows as a loading shift before it shows as a dimensional change.
Where this record comes from
Commissioning reports, service logs and the parameter sheet issued with the line. Machine figures are the quoted bands for the model; process windows follow the Kerke parameter table and are confirmed on a material trial before they become a production setpoint. Where the customer asked not to be named, the country and the application are kept and the company name is not.
Reviewed by the Kerke process team, Nanjing. Case published 9 November 2026.
Send 25–50 kg and we run it on our lab extruder: pellets, running video and a capacity report back in 3–7 days.
Graphite compounding line — the short version
Note on graphite compounding line: the readings in this record come from the commissioning log of the line described, and the settings are the ones that were left with the customer. Treat them as a starting point for your own material, not as a guarantee — the same correction on a different filler grade or carrier ends in a different number.
Related on this site: Extrusion lines by application · Twin screw extruder types · free extrusion line quotation · Wikipedia: Extrusion