Cable compound
Cable Compound Line: PVC, XLPE and HFFR on one platform
Cable compound is heat-sensitive and water-sensitive at the same time, which rules out both long residence time and water contact. That single constraint decides how a cable compound line is configured: the screw, the die and the pelletizer.
- PVC: 140–170 °C, air-cooled strand or hot die-face, no water bath
- XLPE: silane grafting at 190–210 °C, moisture strictly controlled
- HFFR / LSZH: 50–60% ATH or MDH, two-stage, low-shear dispersive mixing
Get a costed configuration
Reply within one working day, in English or Chinese.
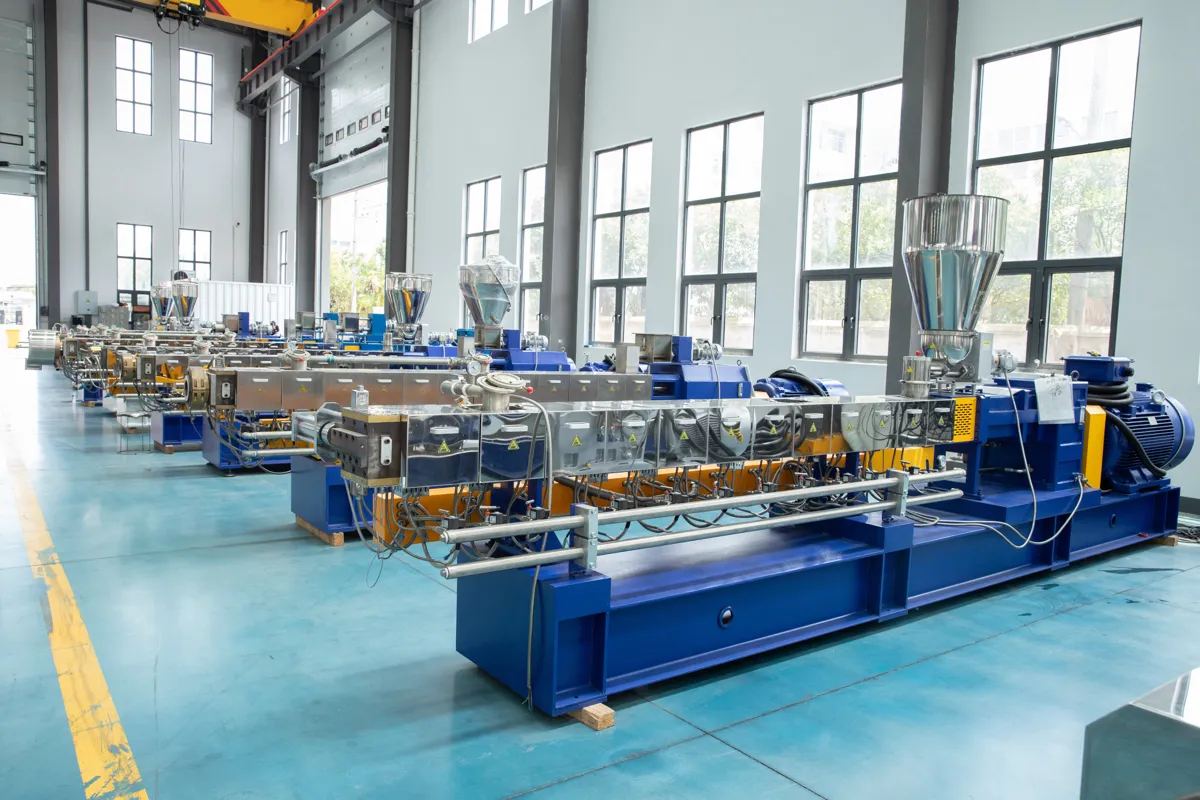
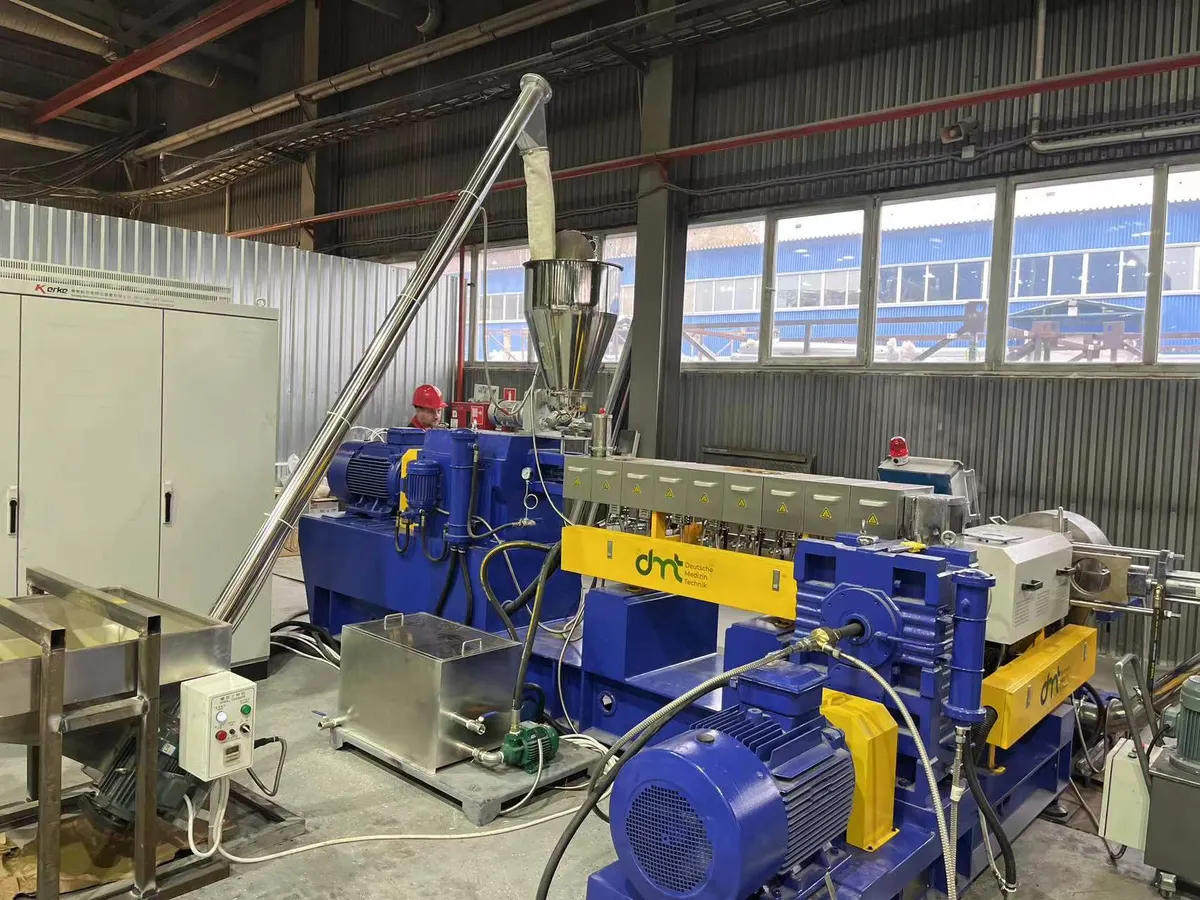
Why one pelletizing method cannot serve all three
A PVC line that runs water through the die is a scrap generator. An HFFR line that shares a water bath with PVC carries moisture into a compound that must stay dry — which is why one cable compound line is configured around a single dominant compound.
PVC: air, not water
PVC at 140–170 °C gels if residence time runs long, and water contact means a drying step you cannot afford. Air-cooled strand or hot die-face keeps the compound dry and the output stable.
XLPE: graft first, catalyse later
Silane cross-linking must be grafted in the extruder and catalysed afterwards. Do both in one pass and the compound starts cross-linking inside the barrel — a stopped line and a scrapped batch.
HFFR: disperse without shearing
Metal hydroxide starts decomposing around 180 °C, so the line has to disperse 50–60% ATH or MDH without the shear that generates local hot spots. A two-stage KTE/SE with a low-shear mixing block is the usual answer on a cable compound line.
- Compound route: PVC dry blend, XLPE grafting, HFFR
- Barrel profile and residence time by compound
- Die-face or strand pelletizing matched to the compound
- Moisture control and drying where the compound demands it
- Gravimetric dosing for ATH / MDH and additives
- Trial report with temperature profile and output
Cable compound line configurations, by compound
| Compound | Barrel temperature | Pelletizing | Line type |
|---|---|---|---|
| PVC (rigid / flexible) | 140–170 °C | air-cooled strand or hot die-face | KTE or KTE/SE |
| XLPE (silane grafted) | 190–210 °C | underwater, dry-cut | KTE with liquid injection |
| HFFR / LSZH | 150–175 °C, low shear | air-cooled, no water | two-stage KTE/SE |
| Semiconductive / sheathing | 160–190 °C | strand | KTE |
Reference values, subject to material trial. Final parameters are set on your own material.
Questions buyers ask before the call
Can one line run PVC and HFFR?
Mechanically yes, commercially rarely: the screw geometry, die and pelletizer are different, and cleaning between compounds is a full day. Most customers buy the cable compound line configured for their dominant compound and quote the second configuration as a change kit.
How do you keep HFFR from pre-curing?
Low-shear mixing, a short residence time after the side feeder, and a barrel profile that keeps local temperatures under the decomposition onset. The trial report lists the actual profile.
What output can I expect on a 75 mm screw?
For PVC dry blend, roughly 400–700 kg/h depending on formulation and bulk density. For HFFR at 55% ATH, expect 30–40% lower on the same screw. We quote the material-specific number after the trial.
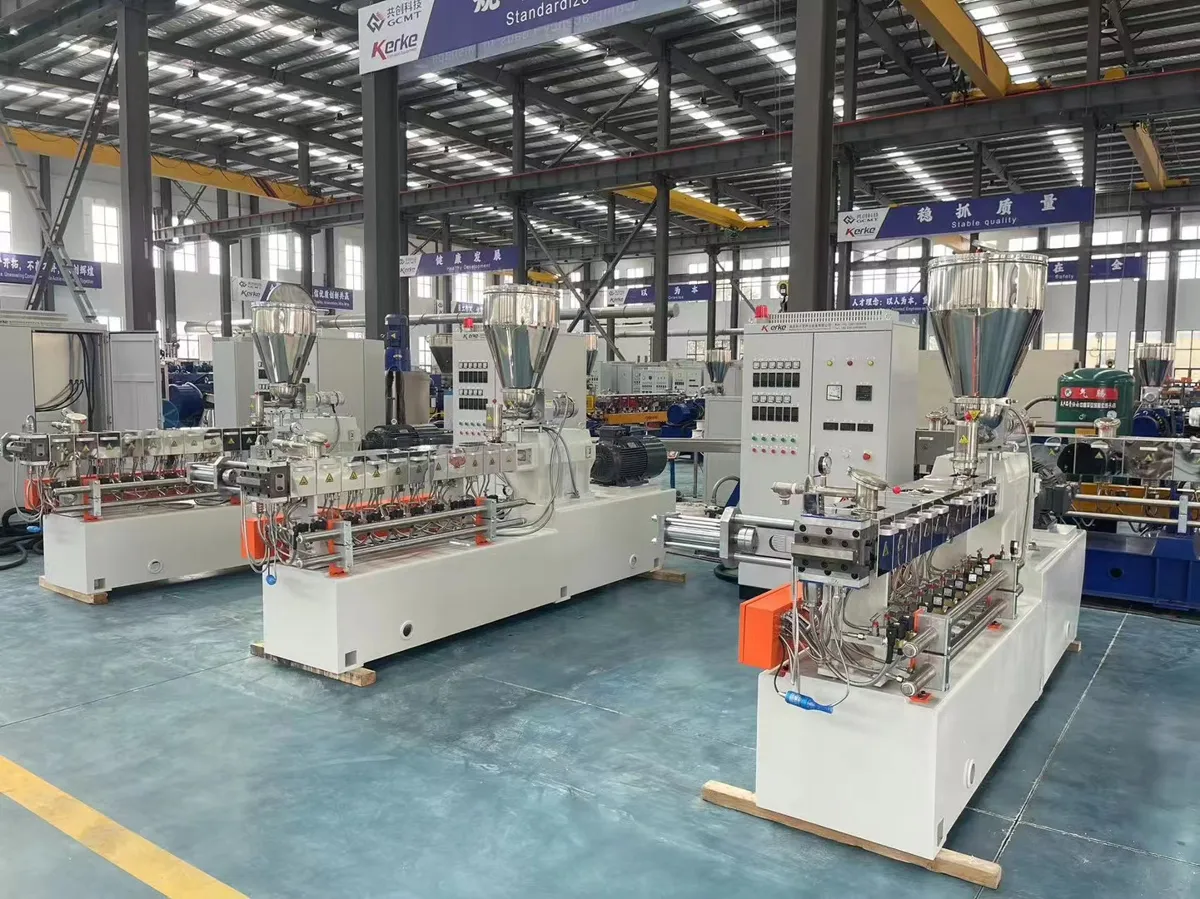
Send your compound and the target kg/h
Tell us the compound type, filler loading and downstream cable size; we reply with the cable compound line configuration and the pelletizing method we would use.