Filler masterbatch
Filler Masterbatch Line: 85–90% CaCO₃, 350–1,500 kg/h
Filler masterbatch is sold by the tonne, so the line is judged on two numbers: how much powder it can swallow, and whether the pellets still feed cleanly in your customer's film line. Both decide the filler masterbatch line output before the extruder is even chosen.
- 85–90% CaCO₃ on a two-stage line; 80–85% on a single-stage twin screw
- Gravimetric feeding and side feeding for high bulk-density filler
- Bimetallic liner and PM elements quoted by wear duty, not hidden
Get a costed configuration
Reply within one working day, in English or Chinese.
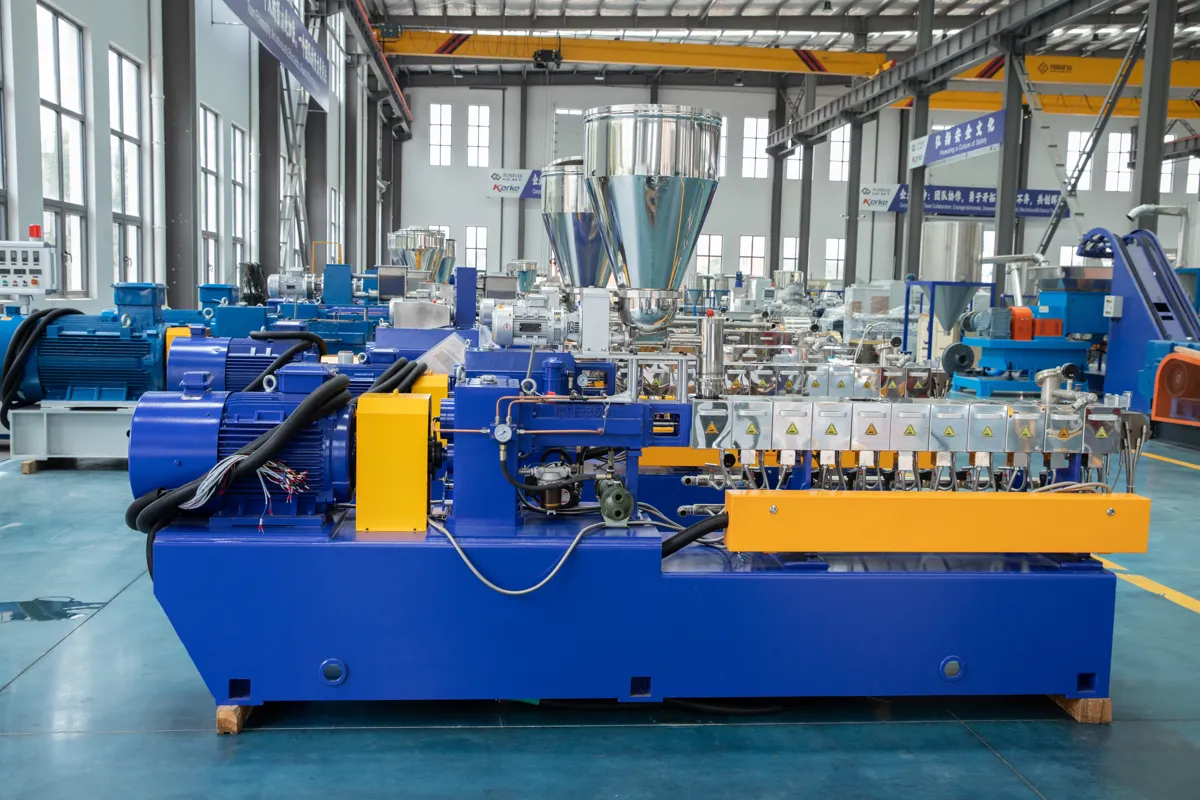
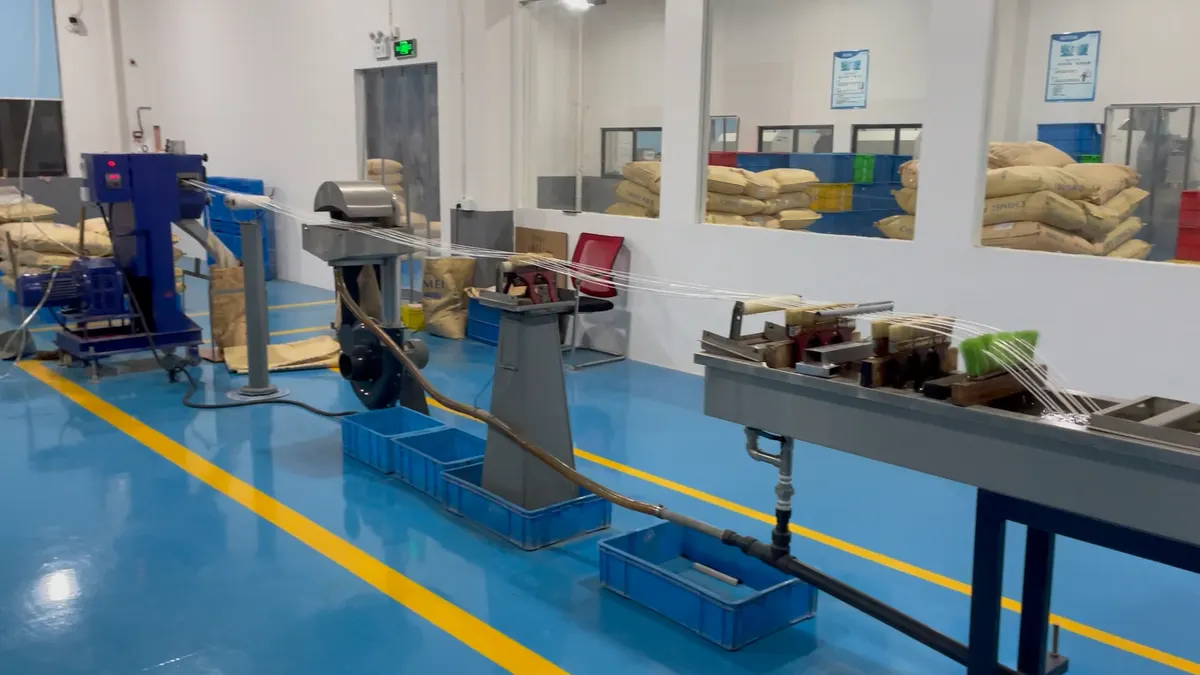
Three decisions that set the output before the screw
Above 85% filler the melt stops behaving like a polymer. Output no longer follows screw speed, and the filler masterbatch line that held 82% will not hold 88%.
Feeding, not melting
CaCO₃ at 1,200 kg/h is a powder-handling problem. Loss-in-weight feeding with an agitator and a correctly sized throat is the first cause of filler masterbatch line output loss — and the cheapest to fix.
Single stage or two stage
Above 85% the melt viscosity rises sharply. A two-stage KTE/SE line splits compounding from pressure build-up, which holds output stable and protects the gearbox.
Wear, priced in
A standard barrel on 85% CaCO₃ wears out in 12–18 months. Bimetallic liner and PM screw elements are specified as a quotation line so the cost is visible from day one.
- Loading ceiling confirmed against your filler grade
- Screw configuration for dispersive mixing
- Vacuum vent at barrel 6–8 for moisture and volatiles
- Water ring or air-cooled strand pelletizing
- Centrifugal dryer, vibrating screen, bagging
- Capacity report with temperatures, screw speed and feeder settings
Reference parameters — filler masterbatch line
| Parameter | Typical value | Note |
|---|---|---|
| Filler loading | 80–90% CaCO₃ / talc | 85%+ needs a two-stage line |
| Screw L/D | 48–52 | custom 28–60 |
| Barrel temperature | 160–200 °C, die 175–190 °C | set by carrier resin |
| Pelletizing | water ring hot die-face / air-cooled strand | water 15–20 °C |
| Output | 100–1,500 kg/h | reference, by screw diameter |
| Recommended model | KTE-65B / KTE-75B; KTE/SE-75/180 above 85% |
Reference values, subject to material trial. Final parameters are set on your own material.
Questions buyers ask before the call
What is the maximum CaCO₃ loading?
85–90% is achievable on a two-stage filler masterbatch line with a bimetallic-lined barrel. Above 88% the melt becomes an abrasive paste: output drops and screw life shortens, so we quote a trial run before committing to a number.
Can one line run 80% and 88% filling?
Yes, with a two-stage configuration and a screw configuration change. A single-stage twin screw sized for 80% will not hold 88% at rated output.
How long does the trial take?
3–7 days for standard filler grades. Send 25–50 kg of your CaCO₃ and carrier resin; we return pellets, a running video and a capacity report.
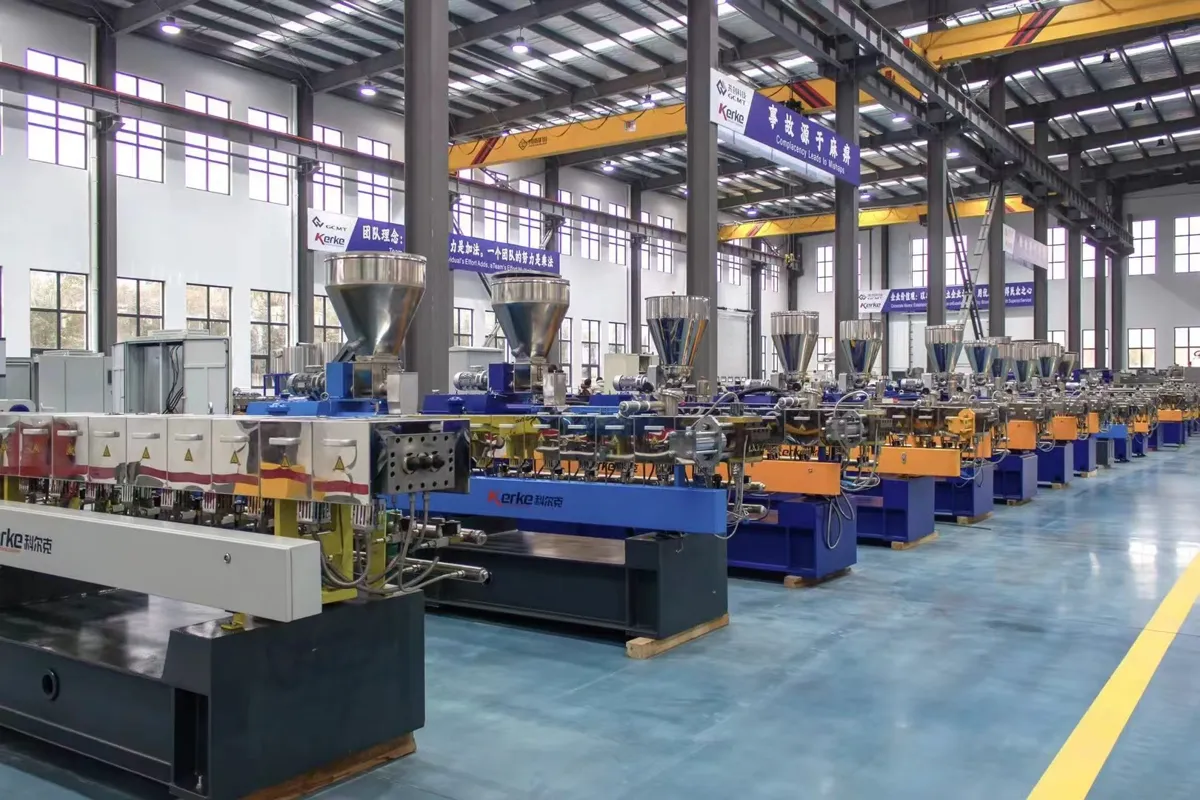
Run your CaCO₃ on our line before you commit
25–50 kg is enough. You get pellets, a running video and the parameters we would guarantee on your filler masterbatch line — in 3–7 days.